Gauge-13 HPPE knit liner
The liner is knitted from high-tenacity UHMWPE (HPPE) yarn at 13 gauge — a fine, dense knit that puts the cut-resistant fibre where the edge meets the hand without the bulk of a heavier glove.
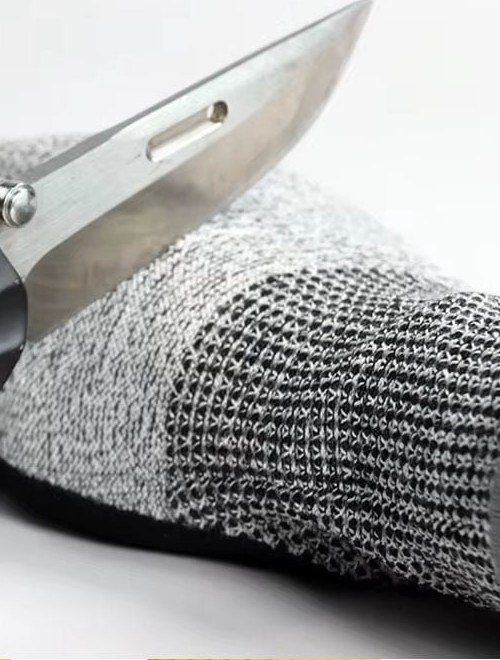
Model GS-48 · UHMWPE (HPPE) knit liner · Nitrile palm coating · Gauge 13
A 13-gauge HPPE knit with a nitrile palm dip — cut, abrasion and puncture resistance with the dexterity to keep working. Part of the HAILIDUN protective line by Shantou Mingda Textile.
Five points
Five points, and the engineering reason behind each one.
The liner is knitted from high-tenacity UHMWPE (HPPE) yarn at 13 gauge — a fine, dense knit that puts the cut-resistant fibre where the edge meets the hand without the bulk of a heavier glove.
The palm and fingers are dipped in nitrile, so the surface resists oil and abrasion and keeps its grip on wet or oily parts, while the back of the hand stays bare knit and the glove keeps breathing.
Cut resistance comes from the fibre, not from the coating: UHMWPE carries the cut and abrasion load while the nitrile adds grip and surface wear resistance. The glove is specified to EN 388 and ANSI/ISEA 105, and the level delivered is confirmed against the test report for the production lot.
A 13-gauge liner is thin enough to pick up, hold and inspect small parts without taking the glove off, which is what decides whether a safety glove is actually worn through a shift.
We spin the HPPE yarn and knit the liner in our own plant in Shantou, Guangdong, so the fibre content and the gauge are controlled at the source rather than in a bought-in glove.
Technical data
What the glove is made of, taken from our product index for model GS-48.
| Model | GS-48 |
|---|---|
| Composition | UHMWPE (HPPE) liner with a nitrile palm coating |
| Liner structure | Knitted liner, 13 gauge |
| Coating | Nitrile, palm-dipped |
| Weight per pair | On request |
Composition, liner structure and gauge are the recorded values for GS-48 in our product index. Weight per pair is set per order and is confirmed with the specification — tell us the sizes and the lengths your programme runs.
Ratings explained
Two standards do the work in a cut-resistant glove, and they are written differently. EN 388 is the European standard for mechanical risks: abrasion, cut, tear and puncture are measured and the result is printed as four digits, with a letter added for the ISO 13997 cut test introduced in the 2016 edition — a code such as 4X42F. ANSI/ISEA 105 is the American standard: cut resistance is reported as a level from A1 to A9, set by the load the blade needs to cut through the sample.
The two scales are not interchangeable. They use different blades, loads and methods, so a glove is tested against the standard the buyer's market uses, and a level is only meaningful with the standard and the edition named beside it. What both scales agree on is the principle: read the level against the work the glove is bought for, not as a number on its own.
| What it decides | EN 388 | ANSI/ISEA 105 |
|---|---|---|
| Scope | Mechanical risks to the hand: abrasion, cut, tear, puncture | Hand protection: cut, abrasion, puncture and impact levels |
| How cut resistance is measured | Coupe test (rotating blade under load) in the 2003 edition; ISO 13997 TDM test from the 2016 edition | TDM test; the result is the load in grams needed to cut through the sample |
| How the result is written | Four digits — abrasion, cut, tear, puncture — plus a letter A–F for the ISO 13997 cut result | A cut level from A1 (lowest) to A9 (highest) |
| Where it is used | Europe, and the markets that follow EN standards | United States, and the markets that follow ANSI/ISEA |
The two cut standards compared
| Standard | Cut level | Load the level stands for |
|---|---|---|
| EN 388:2016 (ISO 13997) | A | 2 N and above |
| EN 388:2016 (ISO 13997) | B | 5 N and above |
| EN 388:2016 (ISO 13997) | C | 10 N and above |
| EN 388:2016 (ISO 13997) | D | 15 N and above |
| EN 388:2016 (ISO 13997) | E | 22 N and above |
| EN 388:2016 (ISO 13997) | F | 30 N and above |
| EN 388:2003 (coupe test) | 1 – 5 | The older five-level coupe scale, still quoted on older listings |
| ANSI/ISEA 105-2016 | A1 – A2 | 200 – 999 g |
| ANSI/ISEA 105-2016 | A3 – A4 | 1,000 – 2,199 g |
| ANSI/ISEA 105-2016 | A5 – A6 | 2,200 – 3,999 g |
| ANSI/ISEA 105-2016 | A7 – A9 | 4,000 g and above |
Cut levels as each standard defines them
| Level band | Typical work | What decides it |
|---|---|---|
| A1 – A2 | Light handling: order picking and packing, assembly of finished parts, handling with occasional light burrs | The occasional sharp edge; dexterity matters more than resistance |
| A3 – A4 | General handling of sharp-edged parts: glass and panel handling, sheet-metal trimming, maintenance | A continuous sharp edge in the hand, so the fibre has to carry the load |
| A5 – A6 | Heavy handling: metal stamping, plate and profile work, demolition and recycling | Heavier cut load plus abrasion, which is where HPPE and steel or glass blends are used |
| A7 – A9 | Extreme cut exposure: heavy plate, blade-adjacent and specialist industrial handling | The highest cut load, normally bought against a specific risk assessment |
Which level for which work
Made to order
The glove is made to order, and the size ladder is set with the order rather than stocked. These are the values we hold today.
In service
Cut-resistant HPPE gloves are specified where the hand meets a sharp edge in normal production — not in an accident, but in the work that happens every shift.
Handling sheet, blanks, profiles and pressed parts where the edge is the hazard and abrasion comes with it.
Moving and fitting glass, panels and laminates: a continuous sharp edge, and a grip that must hold when the surface is wet.
Line assembly, part picking and workshop maintenance, where a thin glove has to stay on for the whole job.
Cartons, strapping, banding and cutters — the everyday cut risks of receiving, picking and dispatch.
This glove is made to conform to the standards listed below, and the level is confirmed against the test report for the production lot. Where a certificate for a specific standard is required, we arrange testing to the customer's requirement.
Test reports are available from our sales team on request, and certificate copies are issued with the sales documents for your order.
A4 and A6 are levels on the ANSI/ISEA 105 cut scale, and the difference is the load the blade needs to cut through the glove: A4 starts at 1,500 g and A6 at 3,000 g, so an A6 glove resists roughly twice the cut load of an A4. In practice that shows up as how long the glove keeps protecting while a sharp edge is dragged across it — A4 for glass, panel and general sharp-part handling, A6 where edges are heavier and the exposure is continuous, such as metal stamping. A higher level usually means a heavier or more blended liner, so the choice is made against the risk assessment rather than simply taking the highest number.
They do not convert directly. EN 388 reports a cut result as a letter from A to F using the ISO 13997 method in its 2016 edition, and ANSI/ISEA 105 reports a level from A1 to A9 using its own TDM test; the blades, loads and procedures differ, so a glove has to be tested against the standard your market uses. EN 388 also prints four digits for abrasion, cut, tear and puncture, while ANSI/ISEA 105 is organised around the cut level plus abrasion, puncture and impact results. Ask for the test report and read the standard and edition it names.
The four digits are abrasion, cut, tear and puncture, in that order, each on a scale from 1 (or 0 if it fails) upward, and a letter after them reports the ISO 13997 cut result of the 2016 edition. A marking such as 4X42F therefore means abrasion level 4, the coupe cut test not performed or not applicable, tear level 4, puncture level 2 and an ISO 13997 cut result of F. Reading a marking this way tells you which tests a glove was actually put through before you read the numbers.
No — cut resistance comes from the knit liner and the fibre in it, not from the coating. What the nitrile palm dip adds is grip and surface abrasion resistance, and it helps on oily or wet parts where a bare knit would slip. This is why we state the liner composition and the gauge alongside the coating: two gloves with the same coating and different liners have very different cut performance.
The liner and the dip are built for industrial service, so the glove can be cleaned — but laundering performance depends on the coating and the cleaning method, and we do not publish a wash-cycle figure without test data for the specific lot. Tell us your laundry or cleaning process and we will confirm what the glove in your specification can take.
Sizes, glove lengths and weight per pair are set with the order, so tell us the size ladder your programme runs and we will confirm the specification against it. This is the reason the size table on this page shows the fields our records leave open rather than a generic ladder: the glove is made to order, and the confirmed size data is issued with the quotation.
The materials are selected and tested for harmful substances — the range is covered by OEKO-TEX® STANDARD 100, which is the test for harmful substances in textiles. Whether a specific glove may be used in contact with food depends on the construction and the local rule that applies to food-contact articles, so tell us the application and we will confirm the construction that fits it.
Yes. The same UHMWPE (HPPE) and aramid fibre systems are used in cut-resistant fabrics, arm sleeves and aprons from our HAILIDUN protective line, and in the reinforcement fabric we supply to hose makers. If your programme needs a cut-resistant layer rather than a glove, tell us the application and we will match the fibre and the structure to it.
Tell us the application, the required weight and the standard you need to meet. Our technical team will come back with a matching fabric, the spec sheet and a quotation.