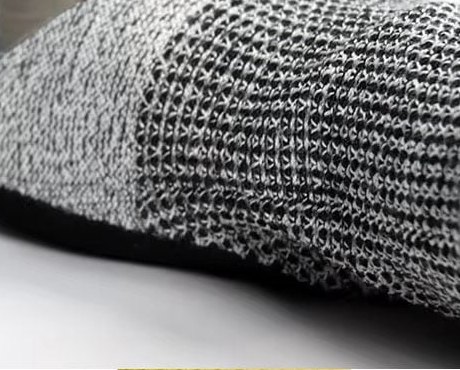
Cut-resistant gloves and glove liners
Knitted gloves and liners for glass, sheet metal and general handling, where the yarn has to resist an edge without making the hand clumsy.
UHMWPE / HPPE · Spun Ne 6s – Ne 40s and filament 200D – 3200D · 100% or wrapped with stainless steel wire / glass fibre
Our UHMWPE (HPPE) yarn family: the ultra-high-molecular-weight polyethylene yarn for cut protection, supplied as 100% UHMWPE, blended with polyester or nylon, or wrapped over a stainless steel wire or glass-fibre core. Built for glove, sleeve, apron and chainsaw-protection programmes.
The material
UHMWPE is ultra-high-molecular-weight polyethylene. Its polymer chains are extremely long and are drawn out along the fibre axis, so load is carried by a near-parallel bundle of chains rather than by a tangled structure. The result is one of the highest strength-to-weight ratios of any commercial fibre, a very high modulus, and excellent abrasion resistance — the combination that makes it the reference fibre for cut-resistant gloves, sleeves and aprons, and for chainsaw-protection fabrics where the yarn has to jam the chain rather than be cut by it.
It is also a light fibre. UHMWPE is less dense than water and substantially lighter than aramid, so a glove or sleeve of a given cut level can be built lighter or with more coverage for the same weight on the hand. Moisture absorption is very low and the fibre is chemically inert, so it does not swell in humid conditions, it resists most acids and alkalis, and it does not rot or support microbial growth the way a cellulosic fibre can.
What UHMWPE is not is a flame-resistant fibre. It melts rather than charring, and a melting fibre can stick to skin — the failure mode that protective clothing standards exist to avoid. For that reason we do NOT offer UHMWPE yarn against any heat, flame, arc or molten-metal requirement, and no flame or heat standard appears in the compliance list on this page. UHMWPE belongs where the hazard is mechanical: cutting, abrasion and puncture.
Colour is the other fixed point. UHMWPE is effectively undyeable — the fibre is highly crystalline and chemically inert, so neither solution dyeing nor piece dyeing is practical in the ordinary sense. The yarn is supplied in its own colour, white as standard and black in regular supply, and colour is used as a functional marker rather than as a design choice. Where a programme needs a colour-coded garment, the colour comes from another fibre in the blend or from the fabric construction.
How it is made
The spun counts in our UHMWPE range are produced on the same two routes we run across the mill — Siro-spun and compact Siro-spun. Both start from drafted staple fibre, and both attack the same weakness: a spun yarn is only as good as the fibres held inside its body, because every fibre end left on the surface is a defect that shows up as pilling, a rougher surface and faster abrasion.
In conventional ring spinning a single drafted strand is twisted into yarn, and the twist runs back into a triangular zone — the spinning triangle — where outer fibres can escape before they are bound in. Siro-spun feeds two rovings side by side through the same drafting zone and the same spinning triangle, so the two strands twist around each other as they form. The yarn that comes out is wrapped rather than combed: fewer fibre ends protrude, and the linear density is more even along the length of the yarn.
Compact Siro-spun adds a compacting stage before twisting. A suction or air current draws the fibre ends back into the yarn body and removes the spinning triangle altogether, so nearly every fibre is trapped inside the structure instead of lying loose on the surface. In practice that gives the tightest surface, the highest yarn tenacity of the two routes and the best evenness — which is the route we use where the cut resistance and the abrasion life of the finished glove matter most.
For the composite constructions the core is fed at the spinning position and bound by the spun sheath, so a stainless steel wire or a glass-fibre core sits inside the yarn rather than being added at the knitting machine. That keeps the core centred, protects it from abrasion and lets the yarn be knitted on ordinary machinery. Cut performance is measured on the finished article, not on the yarn, so the grade a glove or fabric reaches is established by testing it — our test records name the model they belong to rather than a general figure.
| Spinning route | How the yarn is formed | What it gives the fabric |
|---|---|---|
| Conventional ring-spun | One drafted roving twisted into a yarn; the spinning triangle stays open. | The baseline: usable, but hairier and less even, so the surface wears faster and the cut protection is less uniform. |
| Siro-spun | Two rovings drafted and twisted together in the same spinning triangle, then plied. | Lower hairiness and better evenness than ring-spun; a more uniform knitted loop, so abrasion is spread more evenly. |
| Compact Siro-spun | As Siro-spun, with a compacting stage that pulls loose fibre ends back into the yarn body before twisting. | The tightest surface and the best evenness of the three — our route where appearance and abrasion life matter. |
Technical data
The UHMWPE yarns we produce. Where a model carries no recorded count, ply or grade we write On request rather than an estimate.
| Model | Composition | Count | Ply / construction | Rating or key property | Source |
|---|---|---|---|---|---|
| MS-178 | UHMWPE + polyester + stainless steel wire | On request | On request | Cut level D (EN 388) | Index |
| UHMWPE yarn series | 100% UHMWPE; UHMWPE with polyester or nylon; multi-material wrapped over stainless steel wire or glass fibre | Ne 6s – Ne 40s | Single and multi-ply; filament 200D – 3200D | Very high strength and modulus at low specific weight | Yarn & sewing thread catalogue |
The Source column names where each figure comes from: Index is our product information index, Yarn & sewing thread catalogue is the internal catalogue it records. Cut levels are measured on the finished glove or fabric, so the grade a construction reaches is established by testing it; ask our technical team for the current data on the model you plan to use.
Made to order
Count, construction and core are set to the cut level and the comfort the programme needs. UHMWPE is effectively undyeable, so the yarn is supplied in its own fibre colour.
UHMWPE is effectively undyeable: the fibre is highly crystalline and chemically inert, so colour is not a design choice in this yarn. It is supplied in its own fibre colour — white as standard and black in regular supply. Where a garment needs to be colour-coded, the colour comes from another fibre in the blend or from the fabric construction, and our technical team will tell you which route is available for the construction you need.
Our products are made to conform to each standard listed below, in the application it is bought for. Where a certificate for a specific standard is required, we arrange testing to the customer's requirement.
Test reports and certificate copies are available from our sales team on request. UHMWPE is not a flame-resistant fibre — it melts rather than charring — so no heat, flame, arc or molten-metal standard is offered against this yarn; for those requirements a meta-aramid, para-aramid or 3A yarn is the correct choice.
In service
UHMWPE yarn is bought to be knitted or woven into cut protection: gloves and glove liners, sleeves, aprons and chainsaw-protection fabric. The count and construction decide the cut level and the weight on the hand; the core, where there is one, decides what the yarn can do against a powered blade.
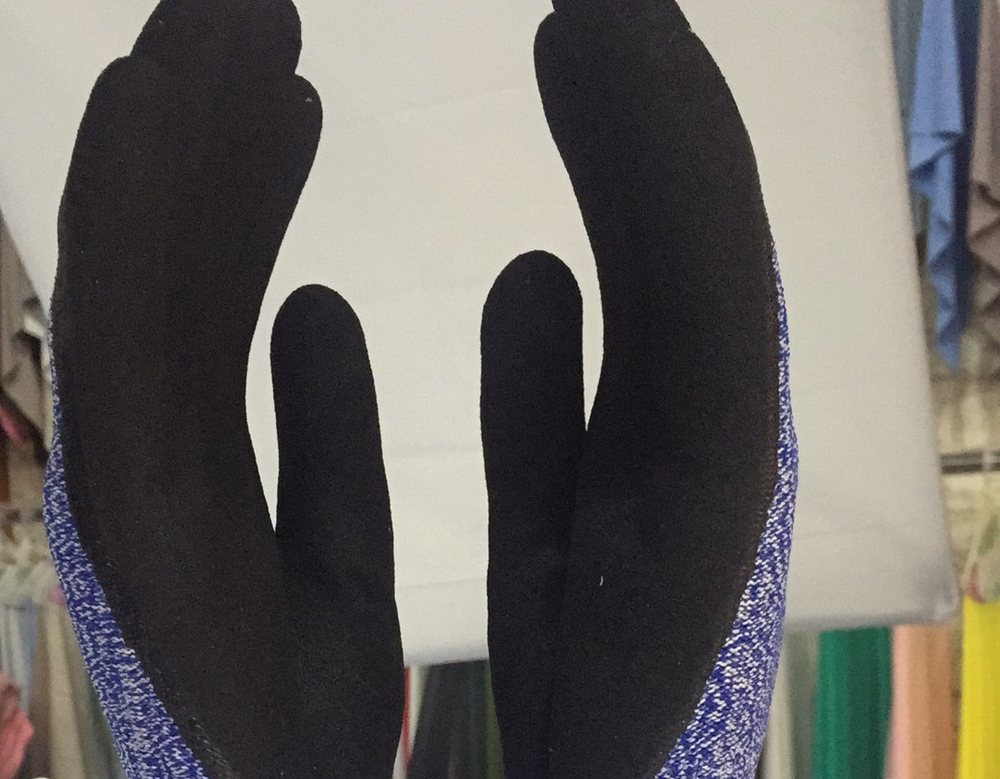
Knitted gloves and liners for glass, sheet metal and general handling, where the yarn has to resist an edge without making the hand clumsy.
Woven and knitted sleeves and aprons for fabrication benches, where a cut-resistant layer covers the forearm rather than the hand.
Steel- or glass-cored constructions that jam a chain instead of being severed — the mechanism behind chainsaw-protective clothing.
They are two different scales and cannot be converted directly. EN 388 is the European standard; on the 2016 version the cut level is a letter from A to F, determined with the ISO 13997 TDM test, while the older 2003 version used a coupe test and returned a number from 1 to 5. ANSI/ISEA 105 is the US standard and its cut levels run from A1 to A9. A programme selling into both markets has to test to both, which is why our records name each result against the standard it came from.
A4 and A6 sit on the ANSI/ISEA 105 scale, and the difference is the load the blade has to reach before it cuts through. In practice A4 covers general handling — glass, sheet edges and light fabrication — where dexterity matters and the hazard is intermittent, while A6 is a heavier grade for sustained contact with sharp edges, plate and metal stamping, and it normally means a heavier or more densely knitted construction. The grade should be matched to the actual task rather than to the highest number available, because the heavier the glove, the more the hand tires.
Because a single fibre cannot do everything. UHMWPE is extremely strong in tension but a powered blade can still part a pure polymer yarn; adding a stainless steel wire or a glass-fibre core inside the spun sheath gives the yarn a hard component that resists and jams the blade, which is the mechanism chainsaw-protective clothing relies on. The core is fed at the spinning position so it stays centred and protected inside the yarn, which also keeps the yarn knittable on standard machinery.
No, and we do not offer it for heat or flame exposure. UHMWPE melts rather than charring, and a melting fibre can stick to skin, so it is not a suitable material against heat, flame, electric arc or molten metal. Its value is mechanical: cut, abrasion and puncture resistance at a low weight. For thermal protection the correct choices are meta-aramid, para-aramid or our 3A yarn, which are all inherently flame resistant and non-melting.
Because the fibre is highly crystalline and chemically inert, which is exactly what gives it its strength and its chemical resistance. The same structure that makes it hard for a blade to cut makes it hard for a dye molecule to penetrate, so neither solution dyeing nor piece dyeing works in the ordinary sense. The yarn is supplied in its own colour — white as standard, black in regular supply — and colour coding in a finished garment comes from another fibre in the blend or from the construction.
It depends on the gauge the glove is knitted at and the cut level the programme has to reach. Our UHMWPE range runs from Ne 6s to Ne 40s for spun counts and 200D to 3200D for filament, and the constructions range from 100% UHMWPE through polyester or nylon blends to steel- or glass-cored yarns. Tell our technical team the gauge and the target cut level and we will confirm the count and construction that fit, with the test data for the model we propose.
Cut performance is a property of the finished article, not of the yarn on the cone, so the grade a programme reaches is established by testing the knitted glove or the woven fabric. Our test records name the model or construction they belong to — for example the EN 388 cut level D recorded for MS-178 — rather than quoting one figure across the range. Where an independent result is needed for your own approval file, third-party test reports can be provided on request.
Tell us the application, the required weight and the standard you need to meet. Our technical team will come back with a matching fabric, the spec sheet and a quotation.